How Gear Blank Machining Allowance Affects Cost
The amount of material left on a gear blank has a direct effect on the work needed to produce the finished part. If there is too much, machinists spend more time removing steel, cutting tools wear faster, and more material ends up as scrap. If there is too little, some surfaces may not clean up properly, and there may not be enough stock left to compensate for distortion during heat treatment.
At PairGears, these details are reviewed as part of the custom gear manufacturing process, based on the customer's drawings and application requirements. Using the least amount of machining allowance does not always result in the lowest cost. The allowance needs to suit the entire production route, including rough machining, heat treatment, and any final grinding.
When comparing supplier quotations, look beyond the blank price. The material, machining sequence, gear geometry, and final accuracy requirements all need to be considered together.
What Is Gear Blank Machining Allowance?
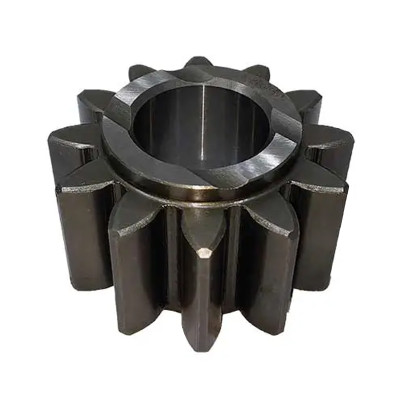
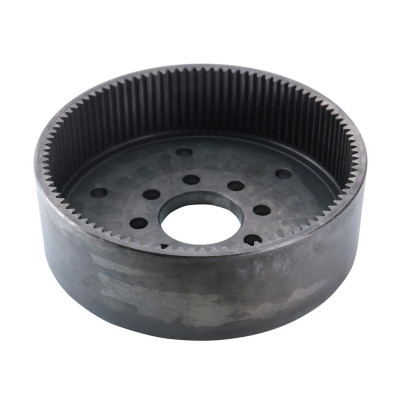
The blank is the piece of material you start from, before the teeth, keyways, chamfers and other final features exist. Allowance is stock deliberately left on particular surfaces so the operations that follow can cut the part to size and finish it.
Where that stock sits depends on the part: outside diameter, bore, faces, hub and shaft journals. If the route includes grinding or hard turning after heat treatment, those surfaces need finishing stock of their own, and it has to be there from the first cut.
Machining Allowance
Material deliberately left on a blank so that later operations can remove it and achieve the required finished surfaces and dimensions.
Dimensional Tolerance
The permitted range within which a finished dimension is allowed to fall. It defines the acceptable finished size, not the amount of material planned for removal.
Allowance and tolerance are two different things, and mixing them up causes problems at quotation stage. Tolerance controls the finished dimension; allowance controls the material planned for removal.
Recommended image: Gear blank before machining beside a finished gear, with the machining stock visually indicated on the blank surfaces.
How Too Much or Too Little Allowance Affects Production
Adding stock may feel safe, while reducing it may look like a way to save material. Neither approach is automatically economical. The allowance has to match the blank condition and the full manufacturing route.
When Allowance Is Excessive
- More machining timeMore stock to remove increases turning, facing and boring time, adding machine hours to the production route.
- Higher tool consumptionHeavy roughing on hard or scaled stock wears cutting inserts faster and adds time for indexing and re-setting.
- More material wasteMaterial removed during machining becomes scrap. On a large alloy-steel forging, the wasted volume can represent a meaningful material cost.
- Greater process demandsHeavy cuts generate heat and cutting force. Thin-walled rings and long shafts may deflect under load, making dimensional control and clamping more difficult.
When Allowance Is Insufficient
- The surface may not clean upForged and rolled blanks can carry scale, a decarburized skin and dimensional variation. Insufficient stock may leave parts of these layers on the finished surface.
- Final dimensions may be difficult to achieveIf the blank varies or the datums are off, a thin machining margin may not leave enough material to correct the error.
- Heat-treatment distortion may be harder to correctHardening can cause growth, ovality or shaft bending. Grinding or hard turning can correct these changes only when suitable finishing stock has been planned in advance.
The practical point: More allowance is not automatically safer, and less allowance is not automatically cheaper. The right amount depends on the blank and the operations the part will actually undergo.
Recommended image: Side-by-side technical illustration showing excessive blank stock and insufficient blank stock, with the machining and cleanup areas identified.
What Sets the Right Machining Allowance?
There is no universal number to apply to every gear blank. The right figure comes from the manufacturing route and the characteristics of the part.
Blank Manufacturing Method
A forging, a cold-extruded billet and a piece cut from bar stock do not arrive with the same size consistency or surface condition, so each needs its own plan. The choice between cold extrusion and hot forging depends on geometry, material, tooling investment and volume.
Material and Part Size
Machinability and hardening response vary between steels. A large ring gear, a long shaft and a thin-walled hub also respond differently to cutting force and machining distortion.
Gear Geometry and Machining Datums
The bore, outside diameter, faces, hub and journals need to line up. Reference surfaces should be established at the blank stage so errors do not carry forward into turning and tooth cutting.
Heat Treatment and Final Accuracy
Allowance must be planned across operations before and after heat treatment. Where grinding follows heat treatment, the drawing and process plan need to identify the surfaces to be finished and the stock reserved for correction.
Not every gear needs grinding. The allowance should match the route the part actually takes, rather than adding extra stock for an operation that is not required.
Recommended image: Gear blank machining process showing blank preparation, turning, heat treatment and final grinding as applicable.
How Allowance Affects the Total Cost
The blank price is the number buyers often look at first, but it does not show the full production cost. Compare the complete route instead.
| Cost Factor | How Allowance Can Affect It |
|---|---|
| Raw material | A bigger blank means more steel bought than the finished part contains. |
| Machining time | More stock to remove usually means longer machining cycles. |
| Cutting tools | Longer cutting wears inserts faster and adds tool changes. |
| Heat-treatment finishing | Without enough stock, distortion cannot be ground out where finishing is specified. |
| Scrap and rework | Poorly planned allowance may lead to incomplete cleanup, dimensional problems or a rejected lot. |
| Lead time | Extra cutting and corrective operations can extend the delivery schedule. |
These factors sit behind custom precision gear cost, together with material, heat treatment, accuracy, quantity and inspection requirements.
What to Confirm Before You Order
You do not have to calculate the machining allowance yourself. The manufacturer needs enough information to review the blank and the production route; the figures can then be evaluated against those requirements.
| Information to Provide | Why It Matters |
|---|---|
| Latest gear drawing or 3D model | Sets the finished dimensions, tolerances and reference features. |
| Material grade and supply condition | Tells the shop how the steel machines and how it will respond to hardening. |
| Blank type, if specified | Shows whether the part starts as a forging, an extrusion, bar stock or another form. |
| Critical machined surfaces | Identifies the bore, faces, outside diameter and other features where stock has to be controlled. |
| Heat-treatment requirements | Sets how distortion will be handled and whether finishing stock is needed. |
| Accuracy and inspection requirements | Determines which dimensions and gear features need to be checked. |
| Sample and production quantities | Allows tooling, setup time and unit cost to be compared realistically. |
| Application and operating conditions | Confirms that the selected manufacturing route suits the gear's actual use. |
If the drawing says nothing about blank dimensions or allowance, state this in the RFQ instead of leaving the field empty. This allows the blank design and machining sequence to be reviewed before the price is fixed.
For more RFQ preparation guidance, see what information is needed for a custom gear quote.
Recommended image: Buyer RFQ preparation scene with a gear drawing, material specification, blank type, heat-treatment requirements and inspection checklist.
How PairGears Reviews Gear Blank Requirements
On a custom gear job, the blank is reviewed with the rest of the production plan rather than on its own. PairGears looks at the drawing, material, quantity, machining requirements, heat treatment and inspection scope.
Three questions need to be answered during the review:
Enough Stock for the Route?
Is there enough material on the blank for every machining and finishing operation in the route?
Can Excess Stock Be Reduced?
Can the excess stock come down without putting dimensions or process stability at risk?
Do Requirements Match the Application?
Do the material, heat treatment and inspection requirements line up with what the finished gear has to do?
For custom cylindrical gears and shafts, sending the drawing and operating conditions early lets blank design, machining route and inspection requirements be reviewed together. You can learn more about PairGears' custom cylindrical gears and shafts and its gear accuracy control process.
Recommended image: PairGears engineer reviewing a gear drawing beside a machined gear blank, with measuring equipment visible.
Frequently Asked Questions
Is a bigger allowance always safer?
No. Stock gives the shop room to cut and to correct, but beyond a point it adds material cost and cutting time. The right amount depends on the blank process, geometry, steel and what happens after heat treatment.
Does the blank manufacturing method affect machining allowance?
Yes. Forgings, cold extrusions and bar stock arrive with different consistency and surface conditions, and they carry different tooling costs and volume thresholds. These factors shape the operations that follow.
Should machining allowance be planned before heat treatment?
Yes. Allowance should be planned across the complete route. Some material is removed before the furnace, while some remains for correction afterward. The amount depends on expected distortion and whether grinding or another finishing step is specified.
Can buyers specify machining allowance on the drawing?
Yes, when the design or manufacturing specification defines it. If you are unsure, state the finished requirements clearly and describe the intended blank. The manufacturer can review the allowance against the production route.
What information is needed for a gear blank quotation?
Provide the latest drawing revision, material grade, blank dimensions or blank type, heat-treatment requirements, finished accuracy, quantity and application details. Sample photos or the physical part can help clarify missing information.
Conclusion
On the blank drawing, machining allowance may look like a small detail. In production, it affects cutting hours, tool consumption, finishing options, scrap risk and delivery time. Excessive stock increases machining work and material waste; insufficient stock can leave surfaces unfinished or make heat-treatment correction difficult.
The workable approach is to set the allowance from the production route outward: how the blank is made, what material it uses, how the part behaves during machining, what may happen during heat treatment, and what final accuracy it must achieve. A complete drawing and clear production requirements allow this review to happen before the price is fixed.
Need a Gear Blank and Machining Route Review?
Send PairGears your latest drawing, material requirements, blank information, heat-treatment requirements and expected quantity. Our team can review the blank and machining route together before quotation.